Precision Verified Catalog
Featured Orthopedic Implants & CoA-Certified Systems
Every lot manufactured in our 60,000 m² cleanroom facility is backed by accredited ISO 17025 laboratory Certificates of Analysis, material heat-lot traceability, and rigorous mechanical validation.
Orthopedic Pedicle Screw Titanium Internal Drive Connection Compatible Universal Spinal Fixation System Precision
Factory Titanium Distal Lateral Humeral Locking Plate Trauma Fracture Orthopedic Bone Implant
Veterinary Orthopedic Implants Model Aluminium Alloy Orthopedic Fracture Surgical Basic Instrument Plate Model
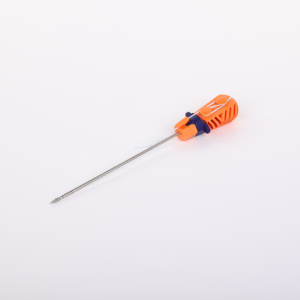
CE Factory Price Suture Anchor 5.5 Titanium Alloy Anchor Ergonomic Handle Orthopedic Instrument Arthroscopy Implants Equipment
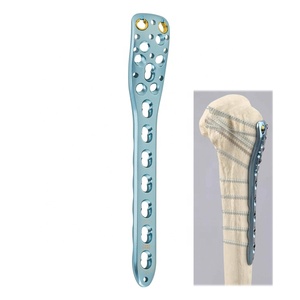
Variable Angle Neck Of Humerus Locking Bone Plate Titanium Orthopedic Trauma Implants
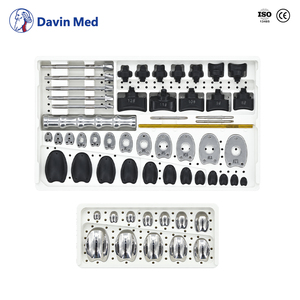
Davin Med Animal Implant Veterinary Orthopedic Hip Replacement System For Canine Severe Patellar Luxation & Trochlear Dysplasia
Direct From ISO 13485 Qualified Manufacturer, Customizable, Disposable Sterile Laparotomy Pack Procedure Set
60,000 m²
Smart Manufacturing Base
450+
Precision CNC Machines
70+
Senior R&D Engineers
20,000
Daily Unit Capacity
Executive Industry Report: Sourcing Orthopedic Implants with Certified Material Traceability
In modern orthopedic surgical device procurement, acquiring top trusted orthopedic implant certificate of analysis (CoA) documentation is no longer a mere administrative checkmark; it is the fundamental cornerstone of clinical safety, legal compliance, and regulatory risk mitigation. For global medical device importers, hospital procurement officers, and OEM brand holders, verifying a factory's Certificate of Analysis goes beyond reviewing raw titanium stock certificates. It requires comprehensive analytical verification encompassing chemical micro-spectrometry, grain-size metallurgical evaluation, dynamic fatigue mechanics, and endotoxin bioload testing.
As regulatory frameworks such as EU-MDR (2017/745), US FDA 21 CFR Part 820, and international ISO 13485 standards intensify audit demands, hospital purchasing committees are strictly scrutinizing supplier lot-level documentation. Implants manufactured without verifiable, lot-specific CoAs expose distributors to severe commercial liabilities—including product recalls, delayed customs clearance, biological osteolysis complications, and catastrophic mechanical hardware failures under dynamic physiological loading.
1. Technical Breakdown: Key Verification Parameters in a Valid Orthopedic CoA
An authentic, accredited Certificate of Analysis generated by an ISO 17025 validated laboratory must detail precise metallurgical, mechanical, surface, and biological testing metrics. Below is the analytical framework required for medical-grade implants manufactured from Ti-6Al-4V ELI (ASTM F136 / ISO 5832-3), PEEK-OPTIMA, and 316L Stainless Steel.
| Testing Domain | Evaluation Parameter | Standard Specification | Clinical & Manufacturing Significance |
|---|---|---|---|
| Chemical Composition | Interstitial Element Limits (N, C, H, Fe, O) | ASTM F136 / ISO 5832-3 (O ≤ 0.13%, Fe ≤ 0.25%, H ≤ 0.012%) | Prevents material embrittlement, ensuring optimum ductility and fatigue resistance under high cyclic physiological loads. |
| Metallurgical Microstructure | Alpha-Beta Phase Grain Size & Alpha Case Inspection | ASTM E112 (Grain Size 5 or finer, Zero Surface Alpha Case) | Guarantees structural uniformity; micro-cracks and brittle surface layers are completely eliminated during high-speed CNC turning. |
| Mechanical Testing | Tensile Strength (Rm), Yield Strength (Rp0.2), Elongation (A5) | Rm ≥ 860 MPa, Rp0.2 ≥ 780 MPa, Elongation ≥ 10% | Confirms that trauma locking plates and spinal pedicle screws resist axial bending, shear failure, and permanent deformation. |
| Fatigue Resistance | Dynamic Load Fatigue Life Cycle Testing | ASTM F2077 / ISO 7206 (Runout at 5,000,000 cycles) | Simulates multi-year patient locomotion, proving implant integrity against micro-motion degradation and fret corrosion. |
| Surface Characterization | Passivation Depth & Anodization Layer Thickness | ASTM F86 Nitric Passivation / Type II Titanium Anodization | Creates a corrosion-resistant bio-inert TiO₂ protective oxide layer, enhancing osseointegration and preventing metal ion release. |
| Biological Cleanliness | LAL Bacterial Endotoxin & Bio-burden Limits | USP <85> (< 20 EU/device, Zero Cytotoxicity ISO 10993-5) | Prevents aseptic loosening, post-operative inflammatory immune responses, and implant-associated bacterial infections. |
At Ortix Medical Devices Co., Ltd., every raw titanium bar stock undergoes incoming Optical Emission Spectrometry (OES) before entering our 450+ multi-axis CNC machining centers. This rigorous raw-material-to-finished-implant lot traceability ensures that when qualified distributors request documentation, they receive a fully compliant, audit-proof CoA portfolio ready for Ministry of Health (MOH) registration.
Future Trend 1: Digital Blockchain-Backed Real-Time CoAs
Traditional paper-based quality certificates are rapidly being phased out by forward-thinking medical device manufacturers. The market is shifting toward digital, cryptographic lot verification. Importers can scan a laser-engraved matrix code directly on the implant packaging to instantly access heat-lot mill test reports, dimensional inspection logs, and ISO 17025 laboratory test certificates stored on immutable digital ledgers.
Future Trend 2: 3D Additive Printing & Micro-CT Certification
With the rapid growth of trabecular porous titanium spinal cages and custom cranial PEEK implants, conventional dimensional measuring machines (CMM) are insufficient. Advanced factories now implement Non-Destructive Micro-Computed Tomography (Micro-CT) CoAs. This certifies internal lattice connectivity, pore size distribution (300–600 μm), and targeted 65% porosity ratios required for optimal vascularization and rapid bone ingrowth.
Future Trend 3: EU-MDR & FDA Import Audit Alignment
Regulatory agencies worldwide are enforcing strict supply-chain accountability for Class IIb and Class III orthopedic medical devices. Importers must demonstrate that their contract manufacturers possess certified ISO 13485 quality systems and provide batch-level biological evaluation reports (BER). Sourcing from vetted OEM factories with complete regulatory CoA support significantly accelerates tender approvals and reduces market-entry lead times.
Future Trend 4: Sustainable Triple-Melt VAR Titanium Metallurgy
Leading orthopedic OEMs are transitioning exclusively to triple-melt Vacuum Arc Remelting (VAR) titanium alloys. VAR metallurgy removes non-metallic inclusions, minimizes micro-segregation, and enhances fatigue resistance. Vetted factory CoAs now explicitly verify VAR processing steps, assuring surgical purchasing directors of superior material integrity during high-load spinal and trauma reconstructions.
Why Global Importers Partner with Ortix Medical Devices Co., Ltd.
Ortix Medical Devices Co., Ltd. stands as a premier global manufacturer specializing in high-precision spine, trauma, joint, sports medicine, CMF implants, and matching surgical instrument sets. Operating across a modern 60,000 m² production facility equipped with over 450 state-of-the-art multi-axis CNC machines, our daily production capacity reaches approximately 20,000 finished units.
Supported by an in-house engineering force of more than 70 R&D biomedical specialists, Ortix Medical offers flexible, one-stop OEM/ODM solutions tailored to global distributors. Key enterprise capabilities include:
- Full Orthopedic Portfolio Consolidation: Single-source supply spanning trauma locking plates, intramedullary nails, pedicle screws, interbody cages, suture anchors, PEEK cranial plates, external fixators, and power tools—drastically reducing supplier fragmentation.
- Flexible Order Quantities (Low MOQ): Optimized inventory management for emerging distributors, allowing low MOQ initial batches and mixed-SKU order combinations across multiple implant lines.
- Turnkey Private Labeling & Laser Engraving: Complete customized laser marking, barcode generation, sterile/non-sterile blister packaging design, and multi-language Instructions for Use (IFU) layout.
- Full Regulatory Dossier Support: Provision of comprehensive technical files, ISO 13485 certificates, FDA establishment registration records, material test reports, and lot-specific CoAs to streamline regional MOH product approvals.
Procurement Knowledge Base
Frequently Asked Questions by Orthopedic Buyers
Clear, authoritative answers addressing quality compliance, CoA validation, manufacturing lead times, and OEM customization.
What is the difference between an ISO 13485 Certificate and a Lot Certificate of Analysis (CoA)?
An ISO 13485 Certificate validates that the manufacturer operates an audited Quality Management System (QMS) compliant with international medical device regulatory standards. In contrast, a Lot Certificate of Analysis (CoA) is a batch-specific laboratory test report detailing the exact chemical composition, mechanical strength, dimensional tolerances, passivation quality, and bio-burden test results for a specific production run of implants. While ISO 13485 proves factory capability, the CoA proves individual product safety.
How does Ortix Medical ensure raw titanium alloy purity before machining?
Every batch of raw medical-grade titanium (Ti-6Al-4V ELI ASTM F136 / ISO 5832-3) entering our facility undergoes rigorous incoming inspection. We utilize in-house Optical Emission Spectrometry (OES) to verify that interstitial elements such as Nitrogen, Carbon, Hydrogen, Iron, and Oxygen remain strictly within medical specification limits. Machining only begins after raw material Mill Test Reports (MTR) are verified and logged into our ERP system.
Can OEM/ODM custom private-labeled implants be issued with certified CoAs?
Yes. Ortix Medical provides fully customized OEM/ODM services, including private-label laser marking, custom surface anodization colors, brand-specific packaging, and personalized IFUs. Every private-labeled order receives a dedicated, lot-traceable Certificate of Analysis issued under your designated product references and quality requirements, supporting local hospital registration dossiers.
What dynamic mechanical testing protocols accompany spinal and trauma implants?
Spinal pedicle screws, anterior cervical plates, and interbody cages undergo dynamic fatigue and mechanical pull-out testing in compliance with ASTM F2077, ASTM F543, and ISO 7206. Our accredited testing laboratory performs static axial compression, dynamic torsional shear, and multi-million cycle dynamic fatigue runout testing to confirm constructs resist mechanical loosening and fatigue failure in clinical environments.
What biological cleanliness testing is performed for sterile vs. non-sterile implants?
All finished implants undergo multi-stage automated ultrasonic cleaning in cleanroom environments to eliminate residual machining oils and particulate matter. For non-sterile products, bio-burden testing confirms low baseline colony-forming units (CFU). For sterile-packaged products, Limulus Amebocyte Lysate (LAL) bacterial endotoxin testing certifies limits below 20 EU/device in accordance with USP <85>, alongside ISO 11137 gamma/EO sterilization validation.
What is the Minimum Order Quantity (MOQ) for mixed-SKU orthopedic shipments?
We understand the financial and logistics challenges distributors face when stocking wide sizing runs of trauma plates or pedicle screws. Ortix Medical supports flexible low-MOQ sourcing models. Distributors can combine multiple product families—such as locking plates, intramedullary nails, spinal cages, and surgical instrument sets—within a single consolidated shipment, minimizing stock holding costs while satisfying clinical demands.
How fast can evaluation samples be delivered for hospital committee approval?
Standard catalog evaluation samples are dispatched within 3 to 7 business days following request approval. Our sample evaluation program allows orthopedic surgeons and procurement leaders to inspect surface passivation finishes, thread pitch precision, dimensional tolerances, and instrument set compatibility prior to finalizing bulk commercial contracts.
How does Ortix Medical assist with local Ministry of Health (MOH) registration audits?
Our dedicated regulatory affairs team provides distributors with complete technical registration dossiers (STED format). This documentation package includes ISO 13485 certificates, FDA registration credentials, raw material batch CoAs, mechanical test reports, biological evaluation studies (ISO 10993), sterilization validation protocols, and surgical technique guides needed for swift MOH approval.